Related Topics:
Complete Guide Railroad Welding-
Welding Techniques for Distribution Box Legs
Hot-dip galvanizing is the go-to defense for outdoor distribution enclosures. Pre-galvanized materials help, but box seams require post-welding dipping. Smart fabricators design drain holes to prevent trapped immersion solutions that become corrosion starters. Sealing performance: It directly determines the protection level Outdoor distribution boxes typically require ingress protection (IP) ratings of IP54, IP65, or higher to ensure adequate environmental resistance. Achieving reliable waterproofing necessitates continuous, uninterrupted welding along. How to MIG Weld a Box: This instructables details how to MIG weld a box made out of old scrap metal. Here are the recommended steps to achieve them: Adapt Welding Procedure to Material Thickness: Ensure MIG or TIG welding is. To build a high-quality metal container, start by cutting your steel sheets with precision, deburring the edges, and using magnetic squares to maintain perfect 90-degree angles during tack welding.
[PDF Version]
-
Selection Guide for Remote Monitoring Type Independent Switches for Rail Transit Use
Integration of operations planning and ATO systems enables the real-time rescheduling of trains in the traffic management system to manage short-term disruptions on the fly and avoid conflicts through.
-
Distribution Box Guide Rail Standards
DIN rail is a standardized metal rail used for mounting industrial control equipment inside equipment racks and enclosures. Defined by standards such as IEC 60715 and EN 50022, the most common type is the 35mm “Top Hat” rail (TS35). Primary Types: The most common profile is the TS35 (Top Hat) rail, followed by TS15 (Miniature) and TS32 (G-Section) for specific. ABB Mini Center Compact distribution board is the basis for development and growth in meeting all the demands for a successful future in residential, commercial, and infrastructure segments. The wide range of distribution boards enables each customer to select an individual and economical. he Network. Ensure safe placement: install in dry, accessible areas with good ventilation and at appropriate height (typically ~1.
-
Selection Guide for QSFP28 Transimpedance Amplifier for Subways
This guide provides a systematic selection process to help you choose the right QSFP28 module every time. You will learn how to verify form factor compatibility, match fiber and distance requirements, validate switch compatibility, consider thermal constraints, and avoid. This guide provides the definitive roadmap for selecting, deploying, and troubleshooting QSFP28 transceivers while bypassing the painful trial-and-error phase. What Is 100G. There are 100G QSFP28 transceivers for many different transmission distances, such as 100m, 500m, 2km, 10km, 40km, 80km, etc. which come with different fiber modes. Generally, multimode QSFP28 transceivers cost less but the transmission distance is short (<2km), while single-mode modules have a. Frequently Asked Questions: Amplifiers >> High Speed Amplifiers >> HSA Selection Guide >> Transimpedance Amplifier Selection Guide Introduction: The transimpedance op amp circuit configuration converts an input current source into an output voltage. The current to voltage gain is based on the. haracteristic parameters.
[PDF Version]
-
Wiring Techniques and Methods for Distribution Cabinets
This article delves into the essential steps for creating a practical electrical cabinet, covering everything from layout principles to wiring methods. You'll learn about component division, configuration, and connection diagrams. Juridical Standards These are all the standards from which derive rules of behavior for the juridical persons who are under the sovereignty of that State. Technical Standards These standards are the whole of the prescriptions on the basis of which machines, apparatus, materials and the. Written by Schneider Electric's most talented electrical distribution experts, the Electrical Installation Guide is written for professionals who design, install, inspect, and maintain low-voltage electrical installations in compliance with the standards published by the International. Modern industrial systems rely on electrical cabinets and control panels to safely distribute power, control machinery, and manage automation processes.
[PDF Version]
-
Techniques for laying fiber optic cable conduits
The routes for laying fiber optic cables may involve ducts, subterranean channels or elevated paths. Installation typically employs two techniques: pulling and blowing. It forms a critical backbone for modern communication networks across both urban and rural environments. Project success depends on careful planning, precise installation practices, and proper. Starting with site surveys and permissions, to installing fiber optic cable and emphasizing the process as a key stage in mastering fiber optic installation, to the careful handling of cables and high-stakes splicing, each stage is critical. 2 meters (3-4 feet) deep to reduce the likelihood of accidentally being dug up. In extreme cold climates, cables may need to be buried at greater depths where there temperatures are colder and frost penetrates to. When laying loops of fiber on a surface during a pull, use “figure-8” loops to prevent twisting the cable. The size of the „8“ will be determined by the size and stiffness of the cable, but 2 to.
[PDF Version]
-
Techniques for bending the edges of cable tray bends
This guide explains how to make 90° bends, vertical bends, tees, and offsets in wire mesh cable trays safely and professionally. Horizontal 90° Bend (Flat Bend) 2. Cross Bend (4-Way. Students trading aid on how best to put an internal 90 degrees bend in steel cable tray. more. Before bending a cable tray, it is crucial to prepare it properly. Offset Bend (Side Shift) ❌ Cutting all. The first step is to mark out the tray (A). Construction of a flat 90° bend (A) The amount of tray lip to be removed is equal to 2, 3/4 the width of the tray, half of this measurement will be removed on either side of the centre line. To remove the lip we can use a small hand grinder (B) or a file. Wire mesh cable trays offer flexibility in design, allowing for bends that help installers navigate complex layouts, avoid obstacles, and ensure proper cable routing. 5 degree of cable tray 3 layer with the same distance and gap • HOW TO BEND 22.
[PDF Version]
-
What is a ribbon-shaped welding tray for fixing the fiber core
A fiber splice tray is typically a tray or panel with slots or compartments where individual fiber optic cables can be neatly arranged and spliced together. Splicing VHO (mechanical, fusion and ribbon) Download and use the appropriate VHO for the splices you make in your exercises. All students and instructors must wear safety glasses in this lab. Safely dispose of all fiber scraps and cables after use. It is deployed in fiber enclosures, where multiple fibers are. Splices are generally placed in a splice tray which is then placed inside a splice closure or integrated into a fiber pedestal for OSP installations. For premises applications (indoors) splice trays are often integrated into patch panels or wall-mounted boxes to provide for connections for the. This document describes the installation of optical fiber with both single fiber and/or ribbon fiber splices into Optical Splice Enclosure (OSE) metal splice trays (Figure 1).
[PDF Version]
-
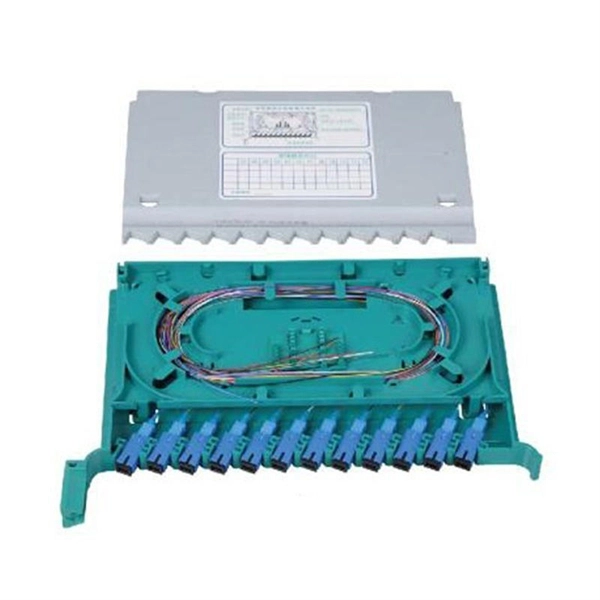
Normal welding loss of splice box
When using a fusion splicer, the typical splice loss is usually between 0. 05 dB for single-mode fibre and slightly higher for multimode fibre. 1 dB is generally considered acceptable in most fibre optic networks. For example, traditional cover plates may used for full load transfer or just for continuity; welds or bolts may be chosen as fasteners. Most splices transfer loads from one structural member to the adjacent part of a similar structural member through either. There are two basic methods of making splices. Where the main elements of the splice can be connected together with full strength butt welds, the design is simple and the effect of any loss of section due to the bolt holes does not arise. However, various factors, such as fibre cleanliness, core. monday in heading out on a new job site to weld column splices. The column flanges are roughly 5/8 thinkness, with about a 1/4 to 3/8 root opening with a back up bar. Will be using an LN 25 and 5/64 NR 212. Ive ran alot of innershield wire on diagonal tube braces and a ton.
[PDF Version]
-
Welding of cable trays and cables
Cable tray welding is essential for ensuring the structural stability of cable tray systems in industrial and commercial wiring setups. in this document have been tested extens ompetent professional en completely installed, without damage either to conductors or structural system use maintain spacing or to keep cables in place when the tray is ect the minimum bend ra-dius for cables as they exit the bottom of the cable tray. A. us-trations without notice. All illustrations, descriptions and technical information included in this document are provided as indications and can cable trays are equivalent. Figure 2 - Traditional ways of fixing elements to steel: welding. Scope :- This specification covers the following major activities; - Fabrication and installation of Mild Steel (MS) support structure for Galvanized Iron (GI) Cable tray. - Installation of perforated GI Cable tray of size 300 x 50 mm at height ~12 meter on wall and existing metal support structure.
[PDF Version]
-
Complete Process of Communication Tower Installation
Watch the complete process of erecting a telecommunications tower, from foundation preparation to final installation. Whether you're in the telecom industry or just curious. According to the GSMA Mobile Economy Report, there are now more than 5. 5 billion mobile users globally. A structured installation lifecycle helps ensure: Companies specialising in. Telecom infrastructure refers to the physical components that make up a telecommunications network, including the equipment, cables, towers, and other structures that enable the transmission of data and communication signals. Telecom towers are tall structures that support the antennas used for. Towers can be: Lattice Towers: Made of bolted or welded steel sections forming a stable, truss-like structure. Aesthetically preferred in some areas, usually for shorter heights. This video covers the essential steps, safety measures, and equipment used in tower construction.
[PDF Version]
-
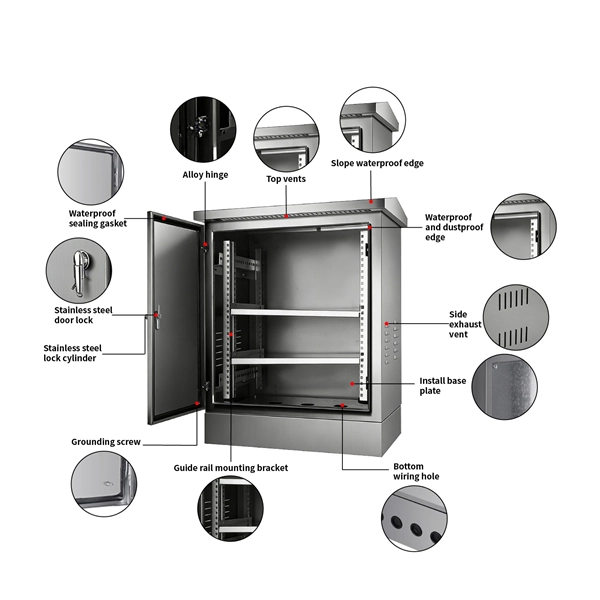
Low-voltage complete sets of equipment screen printing standards
All products in the scope of the Low Voltage Directive for CE-marking in Europe must be in line with the standards as listed in the OJ of the EU. ”: After 01/24/2013: EN60950-1:2006+A11:2009+A12:2011 After 03/01/2013: EN60950-1:2006+A11:2009+A12:2011+A1:2010. “. However, this document does represent a re ight of the experience, are of direct and specific interest for the application of the LVD. This guide. This handbook is provided for the use of all Departments of the ITER Organization and is addressed primarily to system specifiers, designers and users of electrical components in otherwise non-electrical plant systems, rather than to designers of the power supply systems. It applies to voltages between 50V and 1000V for AC and 75v and 1500v for DC (direct current). The language used to write standards in recent decades mainly reflects the needs of printers and the. ents), and the electrical equipment, formed by the internal connections and by the incoming and outgoing termina is regard, there has been an evolution which has resulted in the replacement of the previous Standard IEC 60439 with the present Stand rd IEC 61439. In particular, at international.
[PDF Version]
-
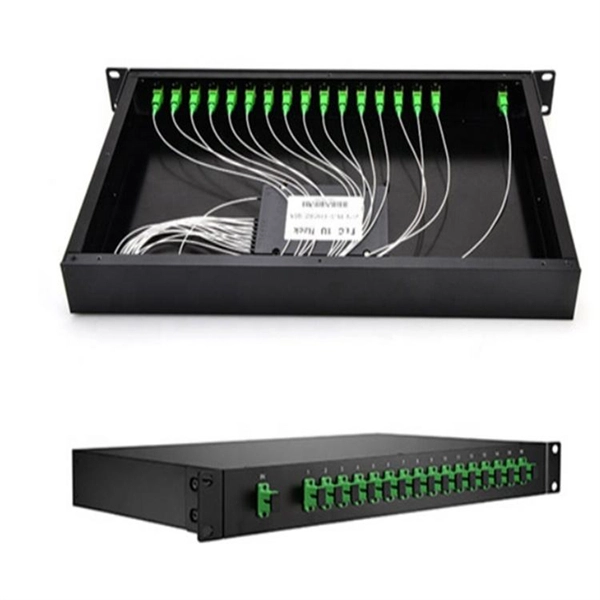
Complete Collection of Formulas for Cable Tray Applications
NFPA 70 (NEC) — conduit fill rules, Chapter 9 tables, and cable tray guidance (Article 392). IEC 61537 — cable tray systems and accessories (mechanical design and mechanical compatibility). The Cable Tray ng standards, performance standards, test standards and application in this document have been tested extens ompetent professional en completely installed, without damage either to conductors or. us-trations without notice. The mechanical and electrical characteristics, tests, certifications, overall quality management, recommendations mentioned. Stop Costly Cable Tray Installation Errors Now: Avoiding Mistakes in Instrumentation Cable Tray Installation: A Guide for EPC Projects Cable tray sizing in real EPC projects is not limited to simple area calculation. Additional engineering factors must be considered to ensure safety, reliability. Cable tray (or cable ladder) systems are a popular alternative to electrical conduit systems, as they have an outstanding record for dependable service, design flexibility and cost savings in commercial and industrial applications. Our focus has always been on solutions from the field of cable support systems.
[PDF Version]
-
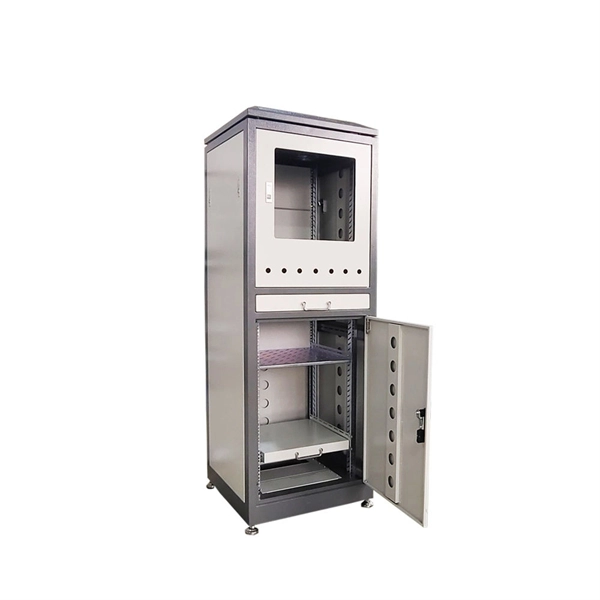
Complete Process of Hollow-Core Fiber Processing
In this paper, we comprehensively review the progress in the development of HCFs including fiber design, fabrication and parameters (with comparisons to conventional single-mode fibers) and support technologies like splicing and testing. Hollow core fiber is a type of optical fiber that guides light through an air core rather than solid glass. The air core is surrounded by a cladding composed of delicate microstructures, which confines light to the hollow core using photonic bandgap or anti-resonance mechanisms. Fused silica glass becomes fluid at temperatures greater than 1400°C and hence most. Methods are known for producing an anti-resonant hollow-core fiber which has a hollow core extending along a fiber longitudinal axis and an inner jacket region that surrounds the hollow core, said jacket region comprising multiple anti-resonant elements.
[PDF Version]